Leave Your Message
-
Phone
-
E-mail
-
Whatsapp
-
WeChat
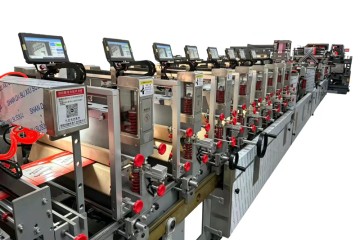
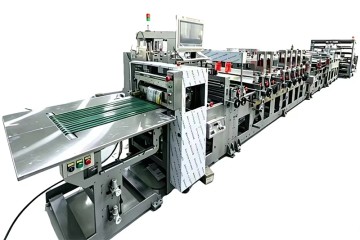
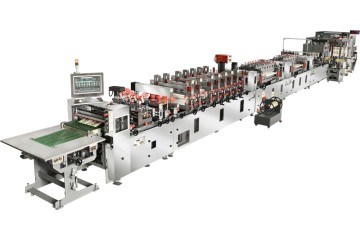
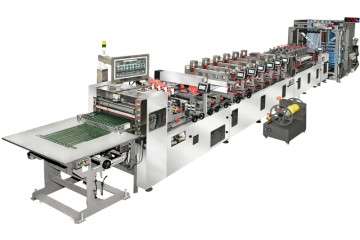
In the modern landscape of industrial manufacturing, the crossover of technology from one sector to another often sparks revolutionary advancements. The engineering principles behind the high-speed, high-tension onion bag making machine have paved the way for sophisticated adaptations in the field of pharmaceutical and medical barrier bag manufacturing. While traditional onion bags are designed for breathability and physical strength to transport agricultural yields, the core mechanics—such as precise tension feedback, high-speed thermal cutting, multi-layer material feeding, and continuous sealing—are highly relevant when re-engineered for medical-grade barrier packaging.
Medical barrier bags require absolute sterile integrity, resistance to moisture, oxygen, and light, and must comply with rigorous cleanroom standards. By applying the robust mechanical architecture of advanced high-speed bag-making lines, manufacturers can achieve unparalleled production efficiency. The transition from processing mesh polymers to handling multi-layer co-extruded films, Tyvek, and aluminum foils demands state-of-the-art servo-driven electronic shafts and integrated CCD vision inspection systems. This technological synergy ensures that medical pouches are produced with zero defects, maintaining hermetic seals that protect critical pharmaceutical ingredients and surgical instruments from contamination.
Ensures consistent material feed without stretching or distorting delicate medical-grade films and Tyvek substrates.
Real-time monitoring of seal integrity, alignment, and dimensional accuracy to eliminate defective pouches instantly.
Microprocessor-controlled heating elements provide consistent hermetic seals required for sterilizable barrier packaging.
The global pharmaceutical packaging market is undergoing a massive shift towards automation and compliance with strict international regulations such as FDA 21 CFR Part 11 and GMP standards. As biological drugs and sensitive medical devices become more prevalent, the demand for high-performance barrier bags has skyrocketed. These bags protect active pharmaceutical ingredients (APIs), diagnostic kits, and implants from ambient moisture, oxygen transmission, and microbial ingress.
To meet these demands, modern machinery manufacturers are integrating smart technologies into their production lines. The adoption of electronic shaft drive systems replaces traditional mechanical chains and gears, reducing vibration, noise, and mechanical wear while dramatically increasing precision. Furthermore, the integration of auto-slitting units, flat-bottom pouch configurations, and multi-functional zipper insertions allows a single machine platform to adapt to diverse medical packaging formats. The flexibility originally engineered into multi-format bag makers is now the benchmark for pharmaceutical packaging lines, ensuring rapid changeovers and minimized downtime.
The application of high-speed, high-barrier bag making machinery in the medical sector is vast and highly specialized. Below are the primary scenarios where these advanced machines deliver critical value:
1. Sterile Medical Device Pouches (Tyvek-to-Film Sealing): Surgical tools, catheters, and syringes require packaging that allows gas sterilization (such as EtO) while maintaining a microbial barrier afterward. The machinery must seal breathable Tyvek to clear polymer films at high speeds without overheating the materials or causing micro-tears.
2. Pharmaceutical Active Ingredient (API) Bulk Bags: Bulk powders and chemical compounds are highly sensitive to environmental factors. Heavy-duty flat-bottom eight-side sealed bags with aluminum laminate layers provide the ultimate barrier against moisture and UV light. These bags require robust sealing bars and precise gusset forming to handle heavy loads without seal failure.
3. Diagnostic Test Kit Packaging: Rapid test strips for medical diagnostics are extremely moisture-sensitive. The packaging process often involves inserting desiccant cards and sealing the pouches under controlled humidity. High-speed three-side sealing machines with integrated punching units ensure clean cuts and hermetic seals to preserve test accuracy.
4. Liquid and Gel Barrier Pouches: Disinfectants, sterile water, and medical gels require high-barrier flexible packaging with secure spout or zipper closures. The machinery must handle complex bottom insertions and multi-layer laminates to prevent leakage during transport and storage.
Xintaihong Machinery Equipment (Guangdong) Co., Ltd. (hereinafter referred to as "Xintaihong"), founded in 2009 and headquartered in Shantou City, Guangdong Province, is a high-tech enterprise integrating R&D, design, production and sales.
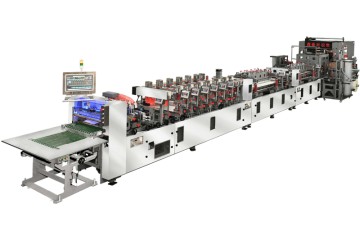
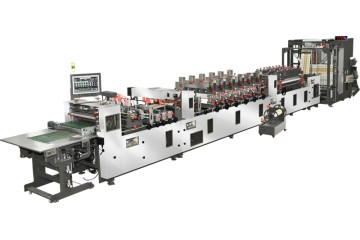
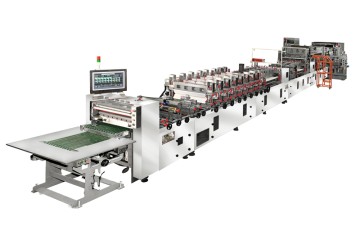
We operate four production workshops and one machining center with a workforce of over 100 employees. Specializing in pouch-making machines, our core product range includes fully automatic high-speed eight-side sealing bag makers, fully automatic high-speed four-side & middle-seal post-forming bag makers, as well as multi-functional fully automatic high-speed three-side sealing machines featuring double stand-up pouches, double zippers and self-inserted bottoms. Backed by robust R&D strength and professional technical expertise, we serve clients across China and worldwide. We deliver comprehensive, optimal automated packaging solutions for new and existing customers engaged in the flexible packaging industry at home and abroad. Our enduring corporate philosophy is to keep innovating and supply cost-effective products to every partner.
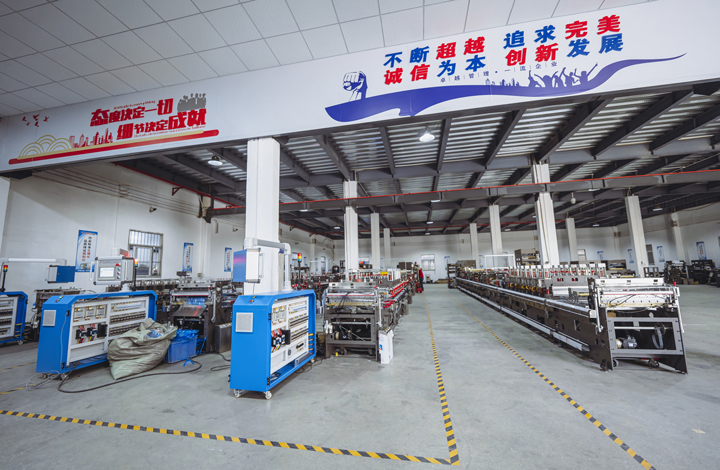
Our self-developed fully automatic bag-making machine for special flat-bottom eight-side seal packaging has obtained certifications from national authoritative institutions and secured national technical patents. Flat-bottom eight-side seal bags, flat-bottom eight-side seal stand-up zipper pouches and flat-bottom eight-side seal carry bags manufactured by this machine rank among the leading products in the packaging sector.
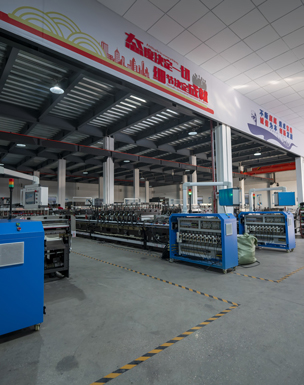
Xintaihong Machinery (Guangdong) is among China’s Top 5 suppliers of bag-making equipment, with eight-side sealing machinery as our flagship specialty. Drawing on over fifteen years of R&D experience and technical accumulation, our machines serve more than 500 clients globally and are exported to over a dozen countries, with over 2,000 units operating stably worldwide. The packaging machinery independently developed and manufactured by our company reaches domestically leading technical standards. It has won widespread acclaim from customers for stable operation, high production speed and low noise output.
Looking ahead, the medical and pharmaceutical barrier packaging sector is moving rapidly towards sustainability. Traditional multi-layer laminates containing aluminum foil are difficult to recycle. Consequently, machinery manufacturers are developing sealing systems capable of handling new mono-material laminates (such as PE-only or PP-only high-barrier films). These eco-friendly films have narrower heat-sealing temperature windows, requiring extremely precise thermal controls and tension management to prevent burning or weak seals.
Additionally, the integration of IoT (Internet of Things) and real-time data logging is becoming standard in pharmaceutical manufacturing. Bag-making machines will not only cut and seal but will also record temperature, pressure, and speed parameters for every single pouch produced, generating a digital birth certificate for each medical barrier bag. This level of traceability ensures complete compliance with global healthcare supply chain regulations, paving the way for safer distribution of life-saving medical products.
Adhering to the corporate tenet of "Harmony & Innovation, Integrity & Courtesy, Unity & Diligence, Co-Create a Shared Future", we take "Supplying premium products and attentive services to customers" as our service mission. As professional equipment developers and designers, we are ready to share more innovative upgrades and new application solutions for bag-making machines with you.